Screening & Conveying Equipment
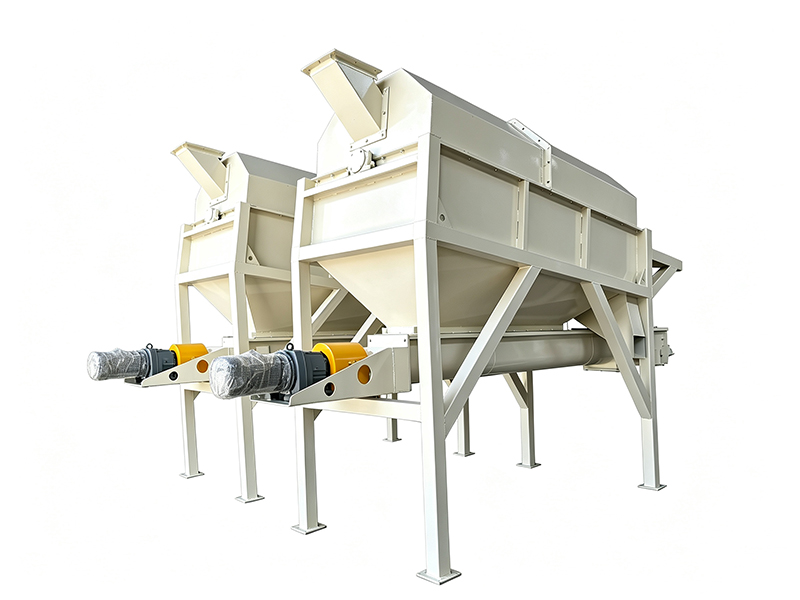
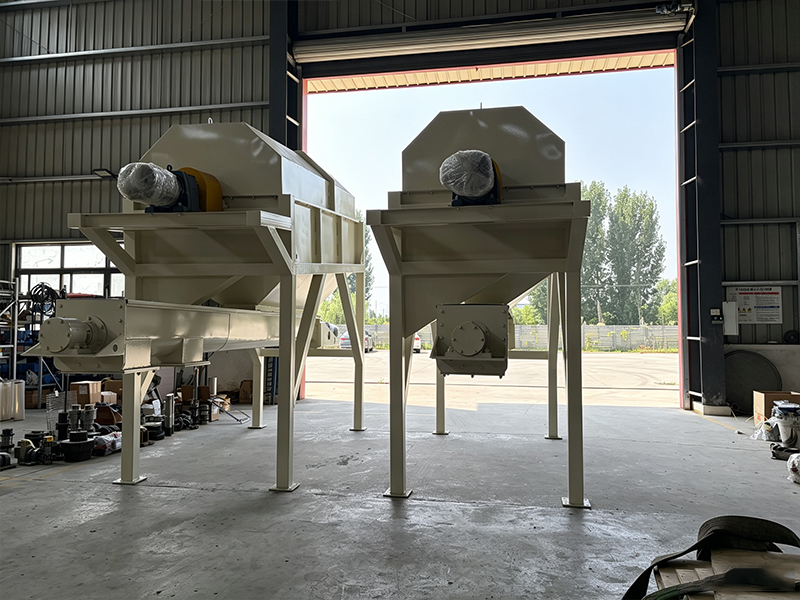
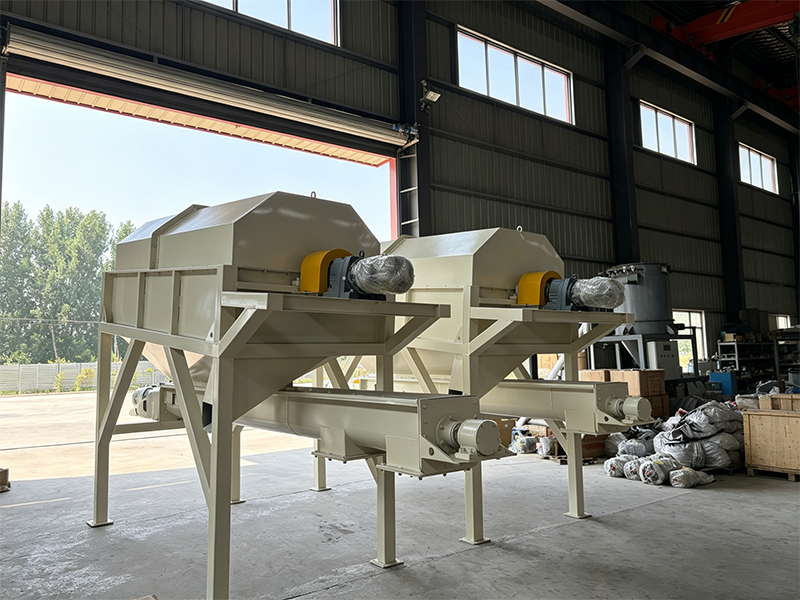
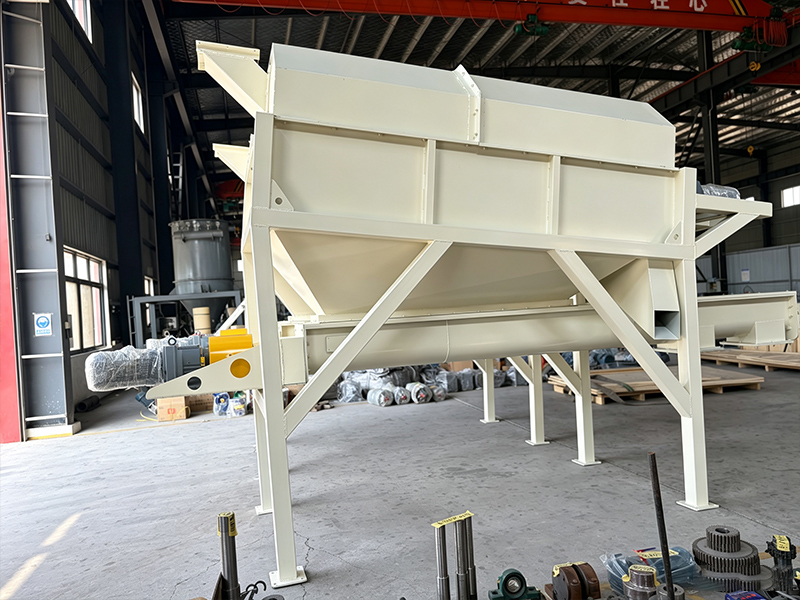
This unit consists of two parallel sealed rotary drum sieve machines integrated with screw conveyors. The upper part is a closed drum screening host equipped with rotating screen cylinder. The tubular screw conveyor is installed underneath. Raw materials enter the drum sieve from the top feeding inlet for screening and impurity removal. Qualified materials fall into the hopper and are conveyed outward by the bottom screw conveyor. It realizes integrated operation of screening, impurity separation and material conveying. The fully enclosed structure reduces dust emission. Two units work in parallel to raise processing capacity. It is widely applied in cleaning and classification of granular and powdery materials. The protective film on motors is for factory storage, which shall be removed before operation.